uni Spiral banner

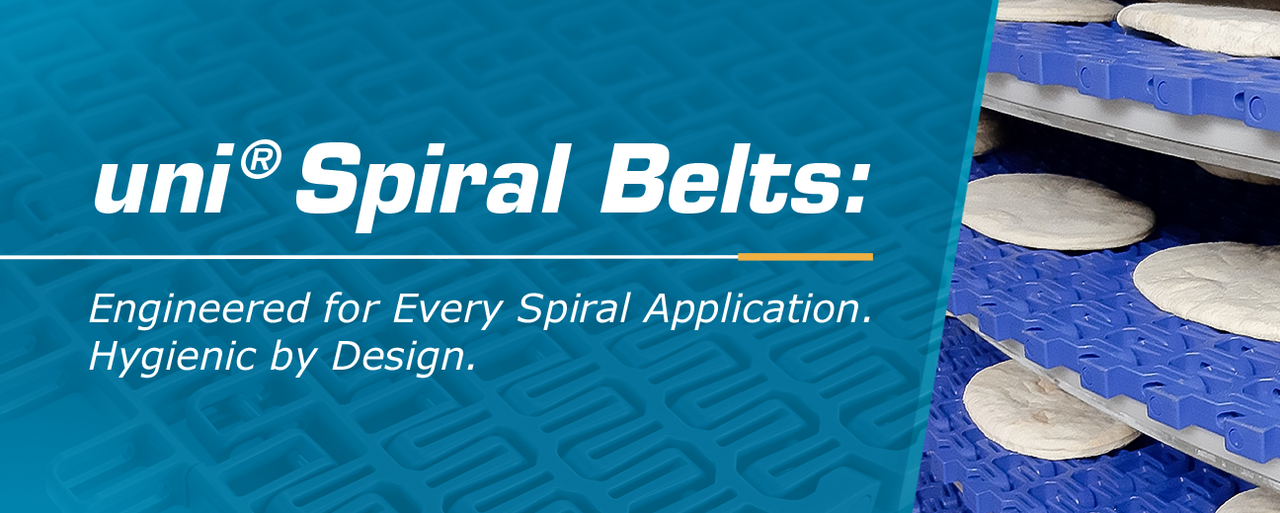
MIR Belting is proud to introduce a new generation of spiral belting solutions in collaboration with uni®, a brand of Ammeraal Beltech. Designed for the most demanding food processing and industrial environments, the uni® Spiral Belts—available in both Friction and Direct Drive systems—combine innovation, hygiene, and reliability to deliver best-in-class performance.

Engineered for Every Spiral Application

Whether you’re cooling, chilling, freezing, proofing, pasteurizing, the uni® Spiral Belts are built to meet your needs:

  • Friction Drive Spiral Belts: Ideal for clean environments and less demanding applications, these belts offer overdrive technology and proven durability.
  • Industry panels on digitalization, logistics innovation, and food safety
  • Direct Drive System Spiral Belts: Featuring the patented uni® Direct Drive System™, these belts deliver smooth engagement, reduced tension, and precise product alignment—ideal for high-performance operations where uptime and product integrity are critical.

Hygienic by Design

With food safety and cleanability top of mind, the uni® Spiral Belts offer:

  • Up to 65% open area for superior airflow.
  • As little as 12% product contact area to reduce contamination risk
  • Easy-to-clean surfaces with no crumb retention

These belts are fully compliant with FDA and EC 1935/2004 standards, supporting your ISO 22000 food safety goals.

Tailored to Your Process

From spiral coolers, chillers, freezers, proofers and pasteurizers the uni® Spiral Belts are available in a range of configurations:

  • uni® Flex OSB & L-OSB: Low surface contact, high beam strength and increased airflow
  • uni® Flex ASB & L-ASB: Robust construction with non-snag belt edges. Larger contact area to support small delicate products.
  • uni® Flex ASB-CS: Curved surface creating a non-stick surface for easy product release.
  • uni® Flex L-OSB Direct Drive: The Direct Drive System provides a smooth unforced engagement and lower belt tension, along with the additional features of the Friction Drive uni® Flex L-OSB belt.

Why MIR? Because This Is Belting Solved.

At MIR, we don’t just supply belts—we solve belting challenges. Our Belting Solved approach is a promise of always-on service, custom-engineered solutions, and trusted support that keeps your operation running 24/7.

  • Custom Solutions: Engineered belts tailored to your exact needs
  • Always-On Support: 24/7 emergency service and rapid response
  • On-Site Optimization: Belt audits, training, and proactive maintenance

With 25 U.S. locations and a team that’s always ready, MIR delivers the reliability, speed, and partnership your operation demands. That’s Belting Solved.

Let’s solve your spiral conveying challenges together.

Contact your local MIR expert or learn more about the uni Spiral Belts today.
Download Brochure here

Proudly Joins the Belting Technology Conference

MIR Belting is excited to announce its participation as a Silver Sponsor at the upcoming Belting Technology Conference (BTC) 2025, the premier industry event dedicated to advancing conveyor belting solutions. Scheduled for May 12–14, 2025, at the Château Élan Resort & Conference Center in Braselton, GA, BTC will bring together top industry experts, manufacturers, OEMs, and end-users to explore the trends and innovations shaping the future of belting technology.

As a trusted partner in the belting industry, MIR provides 24/7 service, expert support, and tailored belting solutions to help customers maximize efficiency and minimize downtime. As part of the AMMEGA group, MIR is committed to innovation, collaboration, and driving progress across the belting industry. Our sponsorship of BTC reflects this commitment.

We’re proud to share that Mark Hambacker, President of MIR, will lead the panel discussion titled: “The Logistics Revolution: Innovating Material Handling for the Future”. This session will explore how cutting-edge belting technologies and logistics strategies are reshaping the supply chain and driving greater efficiency for modern operations.

“BTC 2025 is a great opportunity to connect with industry leaders and explore the future of belting. We’re excited to be part of the conversation and to continue delivering solutions that keep our customers moving forward”, says Mark Hambacker.

BTC 2025 will also feature two dynamic keynote speakers: Tim Hwang, renowned AI expert and author, will present “Belting in the Age of AI & Automation: Adapting for a Sustainable Future,” and Sebastian Mayer, Partner at McKinsey, will deliver insights on “Megatrends Shaping the Belting Industry: Opportunities & Challenges.” These thought-provoking sessions will set the tone for an exciting and future-focused event.

A major highlight of the conference is the BTC Belting Expo, where live equipment displays and interactive demos will showcase the latest advancements in belting products and solutions.

Throughout the event, the MIR team will be on-site to engage with attendees, share insights, and explore new ways to help optimize belting performance.

BTC 2025 will feature:

  • Technical breakout sessions, interactive demos, and hands-on learning
  • Industry panels on digitalization, logistics innovation, and food safety
  • Manufacturing site tours of AMMEGA’s production facilities
  • Networking events to foster collaboration and partnerships across the industry
  • The BTC Belting Expo, bringing products, technology, and people together in one dynamic space

Beyond learning, BTC provides unparalleled networking opportunities, bringing together belting experts and professionals passionate about innovation. Attendees will have the chance to forge new connections, exchange knowledge, and strengthen industry relationships in a dynamic and collaborative environment. Social events throughout the conference will further enhance engagement, offering a relaxed setting to connect with industry leaders and peers.

Join us at BTC 2025 and be part of the conversation driving the future of belting technology. We look forward to connecting with you!

For more details about the event, visit Belting Technology Conference.

BakingTECH banner

We’re excited to join BakingTECH 2025, the premier event for the baking industry, where innovation and expertise come together to shape the future of baking. This year, MIR is proud to showcase our commitment to solving your toughest belting challenges with our #BeltingSolved approach, ensuring your operations run smoothly and efficiently, 24/7.

At BakingTECH 2025, we will highlight our belting expertise and showcase a range of bakery conveying solutions, all available through our extensive network of 25 U.S. locations. Backed by 24/7 service and local support, MIR continues to set the standard in belting solutions and innovation. Some of these solutions include:

  • uni Spiral Direct Drive System™: Learn more
    Built for demanding spiral applications, this cutting-edge system provides smooth operation, energy efficiency, and extended belt life, making it ideal for bakeries needing high-performance spiral conveying.
  • Depanner Belts: Learn more
    Developed for efficient and gentle removal of baked goods from pans, these belts ensure product integrity and are tailored to meet the specific needs of bakery operations.
  • Ropanyl Premium Plus Range: Learn more
    Offering exceptional flexibility, non-stick surfaces, and easy tracking, this belt is perfect for confectionery and snack applications, delivering reliability and efficiency in high-demand processes.
  • Metal Detectable Belts: Learn more
    Designed with safety in mind, these belts minimize contamination risks by being detectable in metal detection systems—a critical feature for food safety compliance.

Join us at BakingTECH 2025 Learn more. To connect with leading professionals in the baking industry, attend inspiring sessions, and visit us at Booth #430 on the Formulation Floor. Don’t miss the opportunity to see our solutions in action, meet our team of experts, and discover how MIR can solve your bakery challenges—every belt of the way. With MIR, it’s Belting Solved

Web Banner ITB

Boost Your Operations with Unmatched Durability and Efficiency

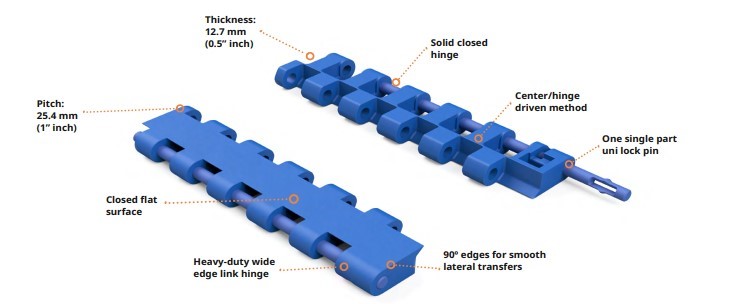
Introducing the uni Industrial Thick Belt (ITB) – a robust and reliable solution for heavy-duty conveyor applications. Engineered to tackle the toughest industrial environments, this modular belt offers exceptional performance with its seamless design, wear resistance, and easy compatibility with existing systems. The uni ITB also offers a hassle-free solution that seamlessly replaces compatible belts from other leading brands.

Boost Your Operations

Why Choose uni ITB?

  • Heavy-Duty Thickness: The 0.5-inch thickness ensures superior load capacity and enhanced wear resistance, ideal for abrasive environments.
  • Easy Integration: Compatible with various products in the market, including Intralox 1400 series and existing sprockets, making it a drop-in solution without the need for conveyor modifications.
  • Simplified Maintenance: Features the uni LockPin system for quick and easy installation, reducing downtime and labor costs.
  • Enhanced Performance: Features the uni LockPin system for quick and easy installation, reducing downtime and labor costs.
  • Interlaceability: The uni ITB’s design allows it to interlace seamlessly with various industry-standard belts, making it capable of replacing any brand on the market without requiring significant changes to your existing setup.

Product Insights

What is the uni ITB?

Key Benefits

Interlace-ability

Ultrafit Two-Part Sprocket

Applications:

Perfect for industries like Bakery, Beverage, Tire, and Corrugated packaging, the uni ITB is your go-to solution for reliable and efficient material handling.

Explore how the uni ITB can enhance your operations, now available at MIR Belting. Call 877-MIR-BELT or request a quote online.

Brochure

Back Contact Us